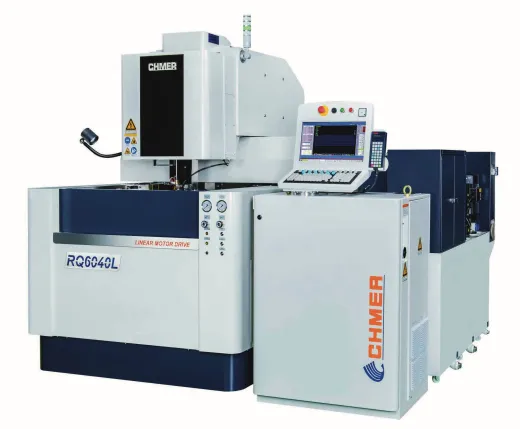
CHMER
CHMER RQ3625L
Wire diameter: Ø0.15–0.3 (Ø0.25) mmCountry of manufacture: TaiwanWeight: 2750 kg
PRICE ON REQUESTDetails →
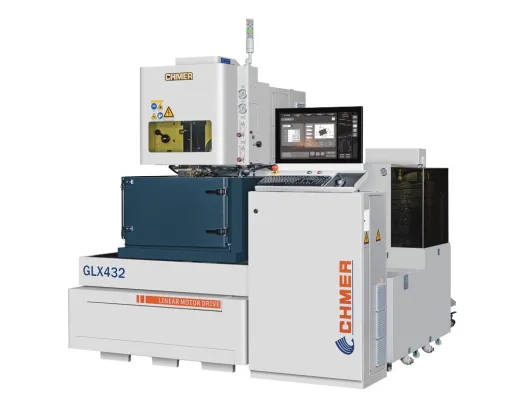
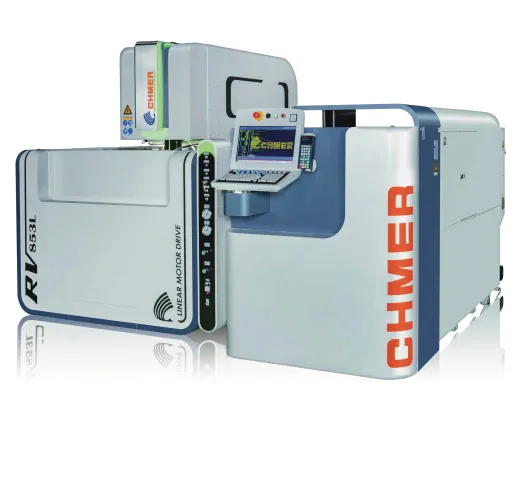
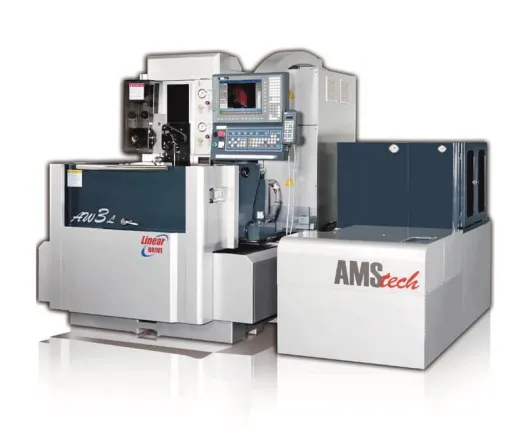
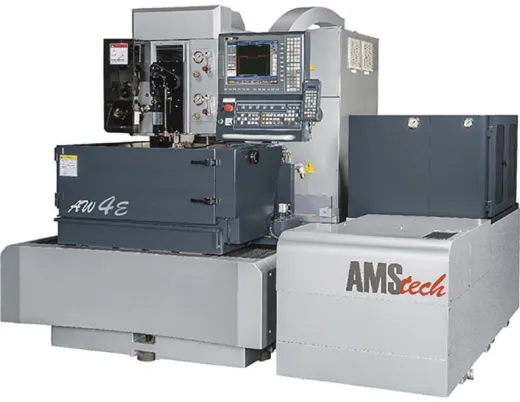
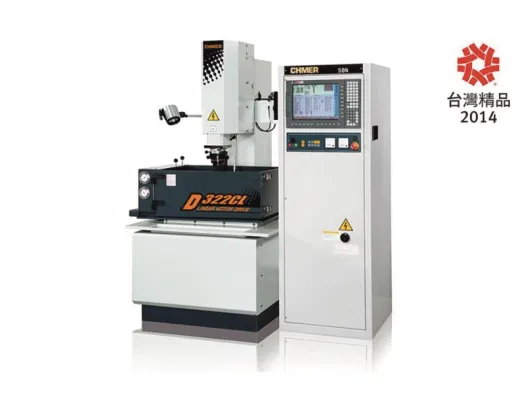
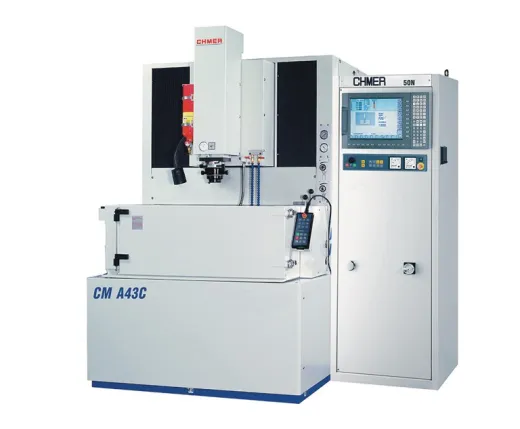
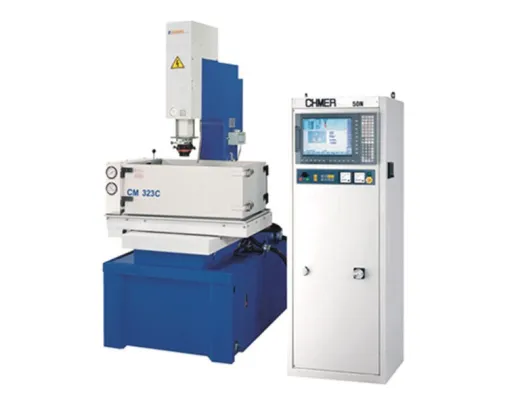
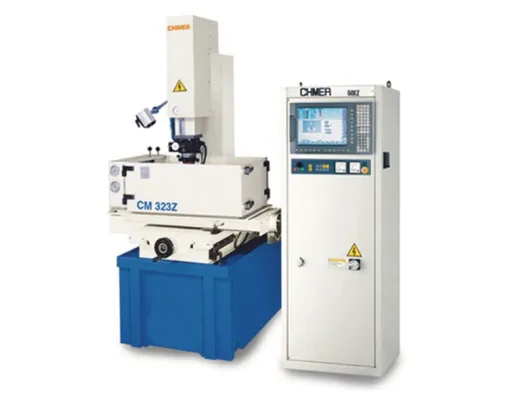
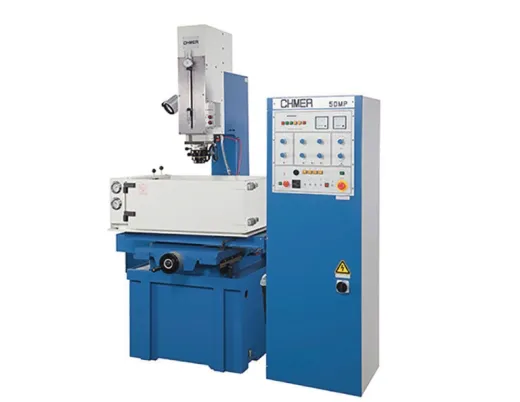
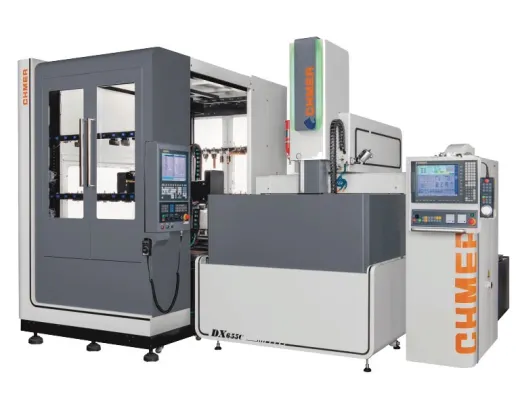
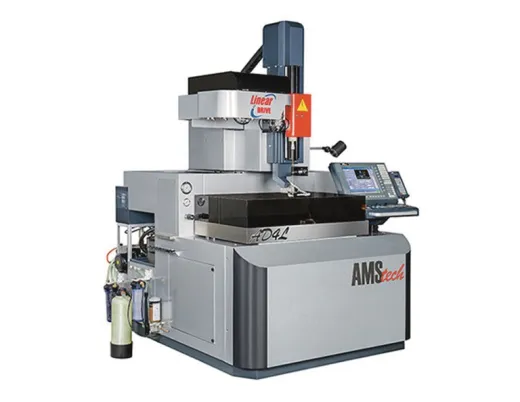
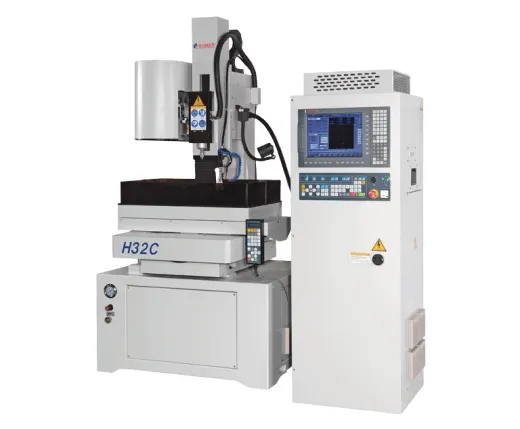
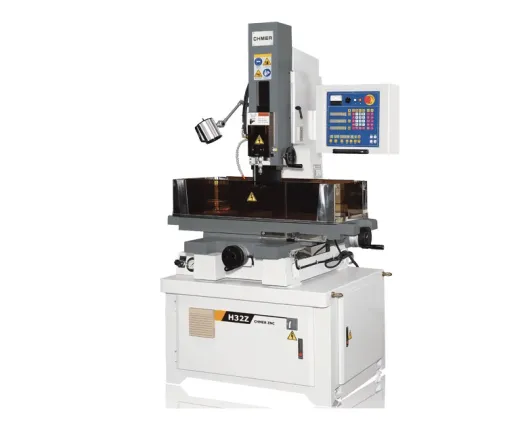
Electrical discharge machining removes metal with a spark rather than a cutting edge: a discharge jumps between the electrode and the part through a dielectric and vaporises a tiny volume of metal. There are no cutting forces, so the hardness of the part does not matter — hardened steel, carbide and heat-resistant alloys machine just like mild steel. There is one limitation, and it is a hard one: the material has to conduct electricity.
| Process | What cuts | What you get | When to choose it |
|---|---|---|---|
| Wire cutting | wire of Ø0.1–0.3 mm | a through contour over the full height of the part, tapered if needed | dies, punches, templates, tooling parts |
| Sinker EDM | a shaped electrode | a blind cavity in the shape of the electrode, with sharp internal corners | moulds, ribs and slots a cutter cannot reach |
| EDM drilling | a tubular electrode of Ø0.2–3.0 mm | a hole in hard material, at an angle if needed | start holes for wire cutting, cooling channels |
The processes do not replace one another, they complement one another. A wire cuts all the way through — it cannot make a blind cavity, which is the sinker machine’s job. And to thread the wire inside a contour that does not reach the edge of the blank you need a start hole — drilled by EDM, because the material is already hardened. That is why the three machines often stand side by side in a shop.
EDM is slower than milling — and that is fine, because it does what milling cannot: it machines a part after hardening, takes carbide, gives a sharp internal corner with no cutter radius, and cuts thin ribs and narrow deep slots without the tool deflecting. If a part can be milled, it is milled. EDM goes where nothing else works.
The equipment in this section comes from the Taiwanese maker CHMER. The range is wide: wire machines run X/Y travels from 360×250 to 1200×800 mm with workpieces up to 5000 kg, sinker machines from 300×200 to 3000×750 mm with workpieces up to 16,000 kg, and drilling machines from 300×250 to 600×800 mm.
| Model | Type | X / Y travels | Z travel | Workpiece, max. | Weight |
|---|---|---|---|---|---|
| CHMER RQ3625L | wire | 360 × 250 mm | 200 mm | 450 kg | — |
| CHMER RQ4025L | wire | 400 × 250 mm | 200 mm | 550 kg | — |
| CHMER RQ5030L | wire | 500 × 300 mm | 200 mm | 600 kg | — |
| CHMER RQ6040L | wire | 600 × 400 mm | 300 mm | 1000 kg | — |
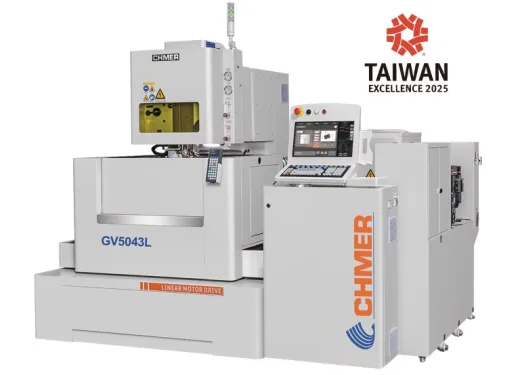
| CHMER GV5043L | wire | 500 × 400 mm | 310 mm | 800 kg | — |
| CHMER NV432L | wire | 400 × 300 mm | 250 mm | 500 kg | — |
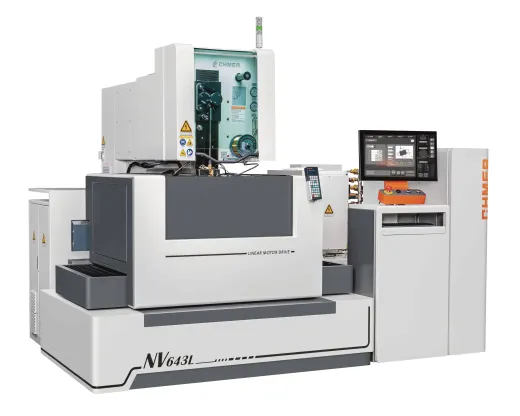
| CHMER NV643L | wire | 600 × 400 mm | 310 mm | 800 kg | — |
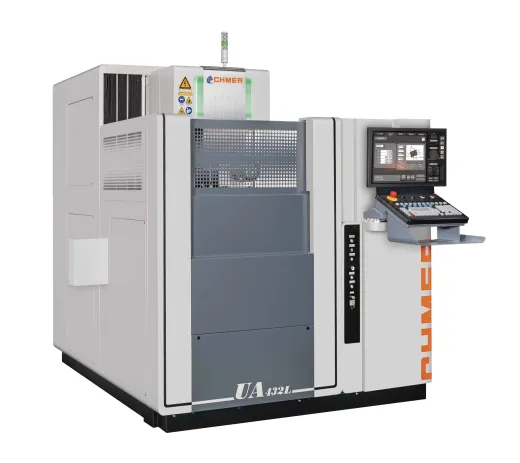
| CHMER UA432L | wire | 400 × 300 mm | 250 mm | 550 kg | — |
| CHMER GLX432 | wire | 400 × 300 mm | 250 mm | 450 kg | — |
| CHMER GLX643 | wire | 600 × 400 mm | 310 mm | 650 kg | — |
| CHMER GX430L+ | wire | 400 × 300 mm | 220 mm | 350 kg | — |
| CHMER GX640L+ | wire | 600 × 400 mm | 300 mm | 600 kg | — |
| CHMER G32S | wire | 360 × 250 mm | 220 mm | 300 kg | — |
| CHMER G43S | wire | 400 × 300 mm | 220 mm | 350 kg | — |
| CHMER G64F | wire | 600 × 400 mm | 300 mm | 600 kg | — |
| CHMER G64S | wire | 600 × 400 mm | 300 mm | 450 kg | — |
| CHMER RX853F | wire | 800 × 500 mm | 300 mm | 2000 kg | — |
| CHMER RX853S | wire | 800 × 500 mm | 300 mm | 1000 kg | — |
| CHMER RX1063F | wire | 1000 × 600 mm | 300 mm | 3000 kg | — |
| CHMER RX1063S | wire | 1000 × 600 mm | 300 mm | 1500 kg | — |
| CHMER RV653L | wire | 600 × 500 mm | 350 mm | 2000 kg | — |
| CHMER RV853L | wire | 800 × 500 mm | 300 mm | 3000 kg | — |
| CHMER RV855L | wire | 800 × 500 mm | 500 mm | 3000 kg | — |
| CHMER RV1063L | wire | 1000 × 600 mm | 300 mm | 5000 kg | — |
| CHMER RV1065L | wire | 1000 × 500 mm | 500 mm | 5000 kg | — |
| CHMER RV1283L | wire | 1200 × 800 mm | 300 mm | 5000 kg | — |
| CHMER RV1285L | wire | 1200 × 800 mm | 500 mm | 5000 kg | — |
| CHMER AW3L | wire | 370 × 270 mm | 260 mm | 500 kg | — |
| CHMER AW5L | wire | 560 × 360 mm | 300 mm | 600 kg | — |
| CHMER AW6L | wire | 650 × 450 mm | 300 mm | 800 kg | — |
| CHMER AW8L | wire | 800 × 500 mm | 300 mm | 3000 kg | — |
| CHMER AW10L | wire | 1000 × 600 mm | 300 mm | 3000 kg | — |
| CHMER AW12L | wire | 1200 × 800 mm | 300 mm | 5000 kg | — |
| CHMER AW4E | wire | 400 × 300 mm | 260 mm | 500 kg | — |
| CHMER AW5E | wire | 500 × 300 mm | 260 mm | 600 kg | — |
| CHMER AW6E | wire | 600 × 400 mm | 300 mm | 700 kg | — |
| CHMER D322CL | sinker | 300 × 200 mm | 250 mm | 300 kg | — |
| CHMER D433CL | sinker | 400 × 300 mm | 300 mm | 350 kg | — |
| CHMER A6040L | sinker | 600 × 400 mm | 350 mm | 1500 kg | — |
| CHMER CM A43C | sinker | 400 × 300 mm | 350 mm | 1000 kg | — |
| CHMER CM A53C | sinker | 500 × 350 mm | 350 mm | 1000 kg | — |
| CHMER CM A64C | sinker | 600 × 400 mm | 350 mm | 1500 kg | — |
| CHMER CM323C | sinker | 300 × 200 mm | 300 mm | 500 kg | — |
| CHMER CM434C | sinker | 400 × 300 mm | 350 mm | 750 kg | — |
| CHMER CM655C | sinker | 600 × 500 mm | 500 mm | 3000 kg | — |
| CHMER CM865C | sinker | 800 × 600 mm | 500 mm | 4000 kg | — |
| CHMER CM1065C | sinker | 1000 × 600 mm | 500 mm | 5000 kg | — |
| CHMER CM1265C | sinker | 1200 × 600 mm | 500 mm | 7500 kg | — |
| CHMER CM1475C | sinker | 1400 × 700 mm | 500 mm | 5500 kg | — |
| CHMER CM1675C | sinker | 1600 × 700 mm | 500 mm | 5600 kg | — |
| CHMER CM1875C | sinker | 1800 × 700 mm | 500 mm | 5800 kg | — |
| CHMER CM2076C | sinker | 2000 × 750 mm | 600 mm | 6800 kg | — |
| CHMER CM3076C | sinker | 3000 × 750 mm | 600 mm | 16000 kg | — |
| CHMER CM323Z | sinker | 300 × 200 mm | 300 mm | 500 kg | — |
| CHMER CM434Z | sinker | 400 × 300 mm | 350 mm | 750 kg | — |
| CHMER CM545Z | sinker | 500 × 400 mm | 500 mm | 1500 kg | — |
| CHMER CM655Z | sinker | 600 × 500 mm | 500 mm | 2250 kg | — |
| CHMER CM240R | sinker | 300 × 200 mm | 300 mm | 500 kg | — |
| CHMER CM380 | sinker | 400 × 300 mm | 350 mm | 750 kg | — |
| CHMER CM545 | sinker | 500 × 400 mm | 500 mm | 1500 kg | — |
| CHMER CM655 | sinker | 600 × 500 mm | 500 mm | 2250 kg | — |
| CHMER DX655C | sinker | 600 × 500 mm | 500 mm | 3000 kg | — |
| CHMER AD4L | drilling | 400 × 300 mm | 300 mm | 900 kg | — |
| CHMER AD5L | drilling | 500 × 300 mm | 300 mm | 1000 kg | — |
| CHMER AD6L | drilling | 600 × 400 mm | 350 mm | 1200 kg | — |
| CHMER H32C | drilling | 350 × 250 mm | 400 mm | 180 kg | — |
| CHMER H64CL | drilling | 400 × 600 mm | 400 mm | 1000 kg | — |
| CHMER H86CL | drilling | 600 × 800 mm | 400 mm | 1200 kg | — |
| CHMER H32Z | drilling | 300 × 250 mm | 345 mm | 120 kg | — |
| CHMER H43Z | drilling | 400 × 300 mm | 345 mm | 450 kg | — |
| CHMER H54Z | drilling | 550 × 400 mm | 345 mm | 1000 kg | — |
| CHMER H75Z | drilling | 700 × 550 mm | 345 mm | 2600 kg | — |
Anything that conducts: steel in any condition including hardened, carbide, titanium, heat-resistant and tool alloys, graphite and copper. Ceramics, plastics and non-conductive composites — no.
By the shape of what you are making. A through contour — wire: the wire passes right through the part. A blind cavity, a rib or a slot with a floor — sinker: the shape is set by an electrode, which has to be made first.
To thread the wire inside a closed contour you need a hole, and the material is already hardened — an ordinary drill will not take it. EDM drilling makes that hole in minutes. The same machine drills cooling channels and holes in carbide.
In wire cutting the wire is consumed and not reused — it is a line in the cost of every part. Besides it you need dielectric and its filtration, and in sinker work the electrodes themselves, made from graphite or copper. Allow for this from the start.
Send your part parameters — we'll select and quote.