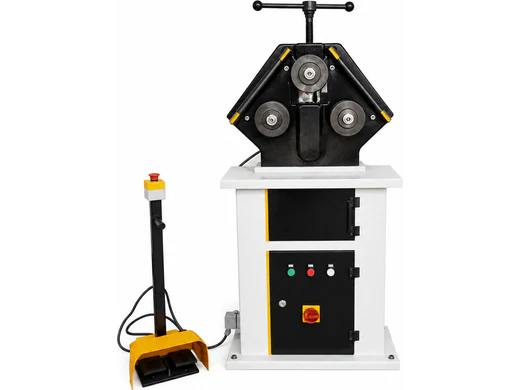
LUNA
LUNA Helix 30
Country of manufacture: ChinaNumber of rolls: 3Shaft diameter: 30 mm
PRICE ON REQUESTDetails →
LUNA Helix, MG and NARGESA MC profile benders and NARGESA CC CNC tube benders: rolling tube, angle, channel and beam to a radius, with 30–530 mm shafts and sections up to 15,000 cm³.
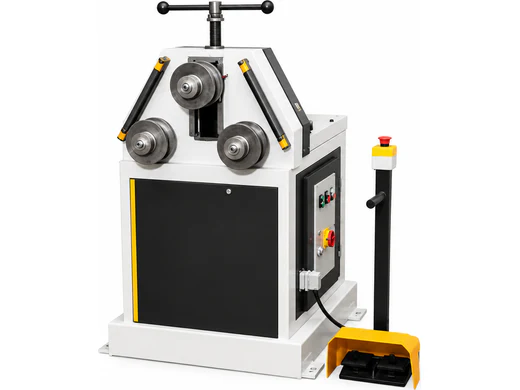
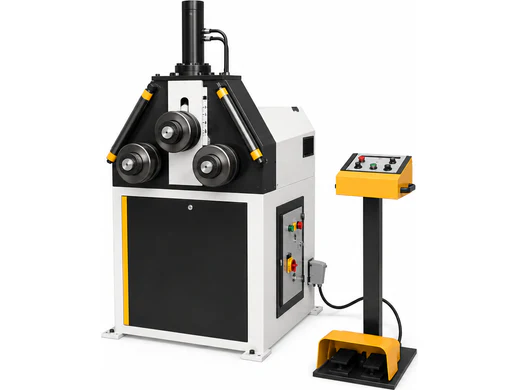
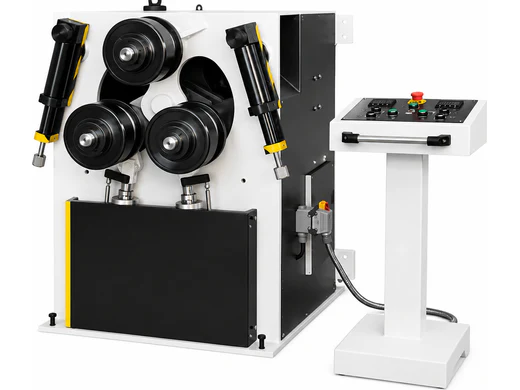
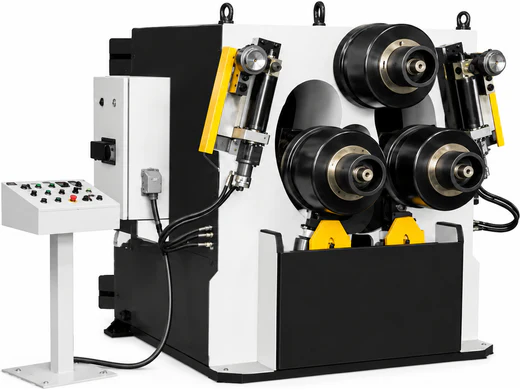
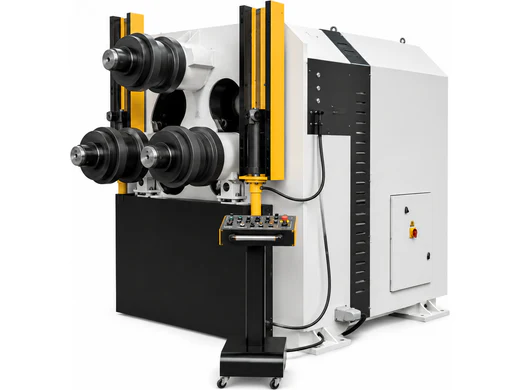

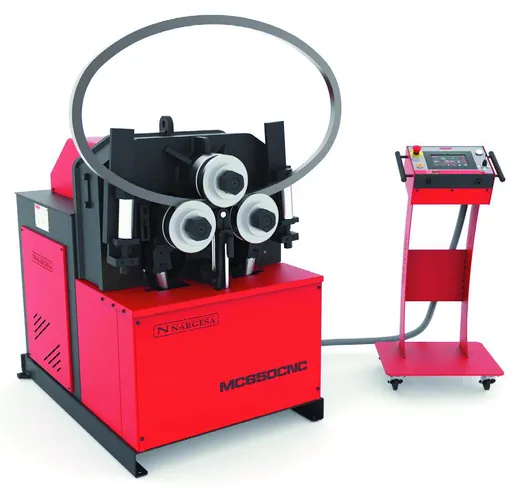
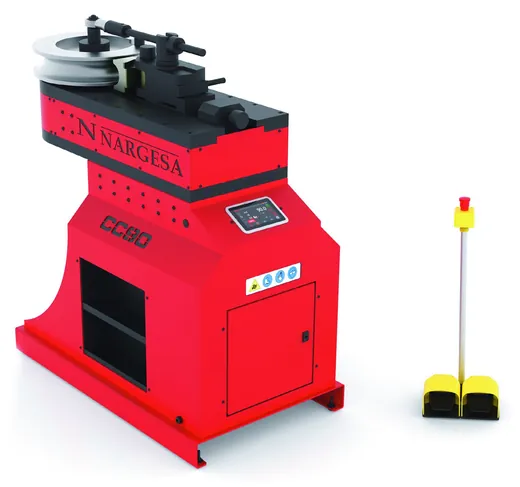
A profile bending machine rolls tube, box section, angle, flat bar, channel and beam to a radius: the workpiece is passed between three rolls and takes the required curvature over several passes. This is how arches, rings, rolled sections, spirals and structural elements are made. The catalog carries our own LUNA Helix machines and Italian MG AR-ARL ones: shafts from 30 to 530 mm and drives from 4 to 218 kW.
These are different machines. A tube bender wraps the tube around a former in one movement, producing a constant radius and an elbow, often with a mandrel inside so the wall does not collapse. A profile bending machine rolls the workpiece between rolls: the radius is set by the roll position and can be large, variable or closed into a ring. Arches, rings, spirals and long sweeping curves need a three-roll profile bending machine. For elbows and batches of identical tube bends the section also has the NARGESA CC CNC tube benders: no mandrel, up to 180°, steel tube up to Ø90 mm.
There are three three-roll lines in the catalog: LUNA Helix, MG AR-ARL and the Spanish NARGESA MC — eight models for tube up to Ø50–101.6 mm, from manual roll adjustment to an ESA S625 CNC. A digital radius gauge is available for the NARGESA benders: 100, 200 and 300 mm arcs, inside and outside radii from 55 to 11,250 mm — the radius is checked without taking the part off the machine.
The capacity of a profile bender is measured not by tube diameter but by the section modulus W in cm³, taken from the tables for your profile. The MG cards give a range: the MG AR-ARL 60 10–18 cm³, the MG AR-ARL 140 45–95 cm³ and the heaviest MG AR-ARL 530 2500–15,000 cm³. It is a range rather than a single figure because the limit depends on the steel grade, the orientation of the section and the radius required.
The same section can be bent in different planes, and W differs between them: a 60×40 box section bent on edge and bent flat are two different jobs for the machine. That is why an enquiry should state not only the section but also exactly how it has to be bent.
Send the section and material grade, the plane of bending, the radius required and the number of parts — we will work out the section modulus, select the model, the rolls and the supports and cost delivery and commissioning. If sheet has to be rolled into a shell, you need plate rolls; for straight bends to an angle, press brakes; and blanks can be cut on band saws or laser tube cutters.
| Model | Shaft diameter | Section modulus W | Roll diameter | Power | Control |
|---|---|---|---|---|---|
| LUNA Helix 30 | 30 mm | — | — | — | Manual |
| LUNA Helix 40 | 40 mm | — | — | — | Manual |
| LUNA Helix 50 | 50 mm | — | — | — | Hydraulic; NC optional |
| LUNA Helix 60 | 60 mm | — | — | — | Hydraulic; NC optional |
| LUNA Helix 80 | 80 mm | — | — | — | Hydraulic; NC optional |
| LUNA Helix 100 | 100 mm | — | — | — | Hydraulic; NC optional |
| LUNA Helix 120 | 120 mm | — | — | — | Hydraulic; NC optional |
| LUNA Helix 160 | 160 mm | — | — | — | Hydraulic; NC optional |
| LUNA Helix 180 | 180 mm | — | — | — | Hydraulic; NC optional |
| MG AR-ARL 60 | 60 mm | 10-18 cm³ | 215 mm | 4 kW | — |
| MG AR-ARL 80 | 80 mm | 20-28 cm³ | 275 mm | 5.5 kW | — |
| MG AR-ARL 110 | 110 mm | 35-55 cm³ | 380 mm | 10 kW | — |
| MG AR-ARL 130 | 130 mm | 40-80 cm³ | 390 mm | 20 kW | — |
| MG AR-ARL 140 | 140 mm | 45-95 cm³ | 400 mm | 20 kW | — |
| MG AR-ARL 160 | 160 mm | 90-160 cm³ | 460 mm | 25 kW | — |
| MG AR-ARL 180 | 190 mm | 100-250 cm³ | 570 mm | 30 kW | — |
| MG AR-ARL 200 | 210 mm | 110-350 cm³ | 630 mm | 30 kW | — |
| MG AR-ARL 250 | 250 mm | 120-700 cm³ | 660 mm | 40 kW | — |
| MG AR-ARL 300 | 300 mm | 150-1000 cm³ | 770 mm | 60 kW | — |
| MG AR-ARL 330 | 330 mm | 180-1100 cm³ | 770 mm | 76 kW | — |
| MG AR-ARL 360 | 360 mm | 200-2000 cm³ | 800 mm | 76 kW | — |
| MG AR-ARL 440 | 440 mm | 250-5000 cm³ | 920 mm | 102 kW | — |
| MG AR-ARL 530 | 530 mm | 2500-15000 cm³ | 980 mm | 218 kW | — |
| NARGESA MC150B | 40 mm | — | — | 0.75 kW | Manual adjustment |
| NARGESA MC200 | 40 mm | — | — | 1.1 kW | Manual adjustment |
| NARGESA MC400 | 40 mm | — | — | 1.1 kW | Manual adjustment |
| NARGESA MC200H | 40 mm | — | — | 1.85 kW | Hydraulic adjustment |
| NARGESA MC550 | 50 mm | — | — | 1.5 + 0.75 kW | ESA S625 |
| NARGESA MC650 | 65 / 80 mm | — | — | 3 + 0.75 kW | ESA S625 |
| NARGESA MC550CNC | 50 mm | — | — | 1.5 + 0.75 kW | CNC ESA S625 |
| NARGESA MC650CNC | 65 / 80 mm | — | — | 3 + 0.75 kW | CNC ESA S625 |
| NARGESA CC60 CNC | — | — | — | 1.1 kW | — |
| NARGESA CC90 CNC | — | — | — | 2.2 kW | — |
A tube bender wraps the tube around a former, giving an elbow of constant and usually small radius, often with a mandrel inside. A profile bender rolls the workpiece between three rolls and produces large, variable or closed radii: arches, rings and spirals. This section has both: three-roll machines and NARGESA CC CNC tube benders.
It is a property of the section taken from the tables: every tube, angle or channel has a W value in cm³, separately for each axis. Find the W of your profile in the plane you are bending and compare it with the range on the machine card. If you are not sure, send us the section and we will work it out.
Yes, if the rolls match the specific section and the radius is not tighter than the wall can take. Thin-walled tube on a tight radius wrinkles on the inside — that calls for a larger radius or a different process. Work this out before buying rather than after.
The price depends on the shaft, the control, the roll set and the supports, and on delivery terms, so it is not listed on the site. Send a request and we will prepare a quotation including delivery, commissioning and training.
Send your part parameters — we'll select and quote.