CHMER
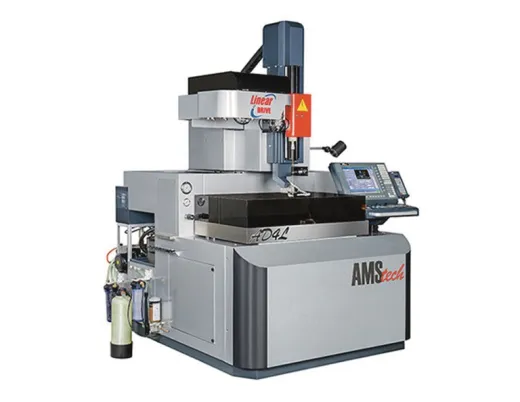
CHMER AD4L
Electrode diameter: Ø0.2–3.0 mmElectrode length, max.: 400 mmCountry of manufacture: Taiwan
PRICE ON REQUESTDetails →
CHMER EDM drilling machines: 10 models, electrode Ø0.2–3.0 mm and up to 400 mm long.
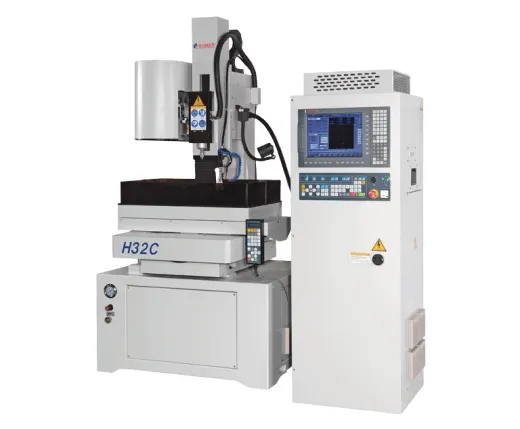
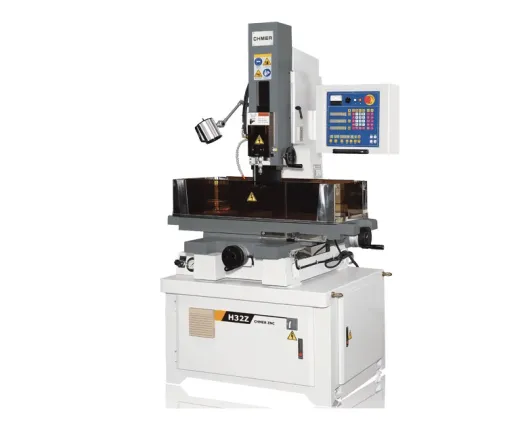
A tubular electrode of 0.2 to 3.0 mm burns the hole by discharge rather than by cutting. The point is that the material is already hardened: where a drill blunts or breaks, the electrode goes through — and with no force on the part, so a thin wall is not pushed out.
Two typical jobs. The first is a start hole for wire cutting: to thread the wire inside a closed contour a hole is mandatory, and an ordinary drill will not make one in a hardened die. The second is holes that are the feature themselves: cooling channels in moulds, holes in carbide, holes at an angle to the surface.
Selection looks at the electrode diameter and length (up to 400 mm in the catalog), the X/Y travels — from 300×250 to 600×800 mm — and the W travel, a separate electrode feed axis. The number of holes decides whether CNC and automatic electrode changing are needed.
This is the simplest machine in the section and often the first one bought alongside an existing wire machine. The neighbouring line is sinker EDM; the full line-up is in the EDM section.
Send your part parameters — we'll select and quote.