NARGESA
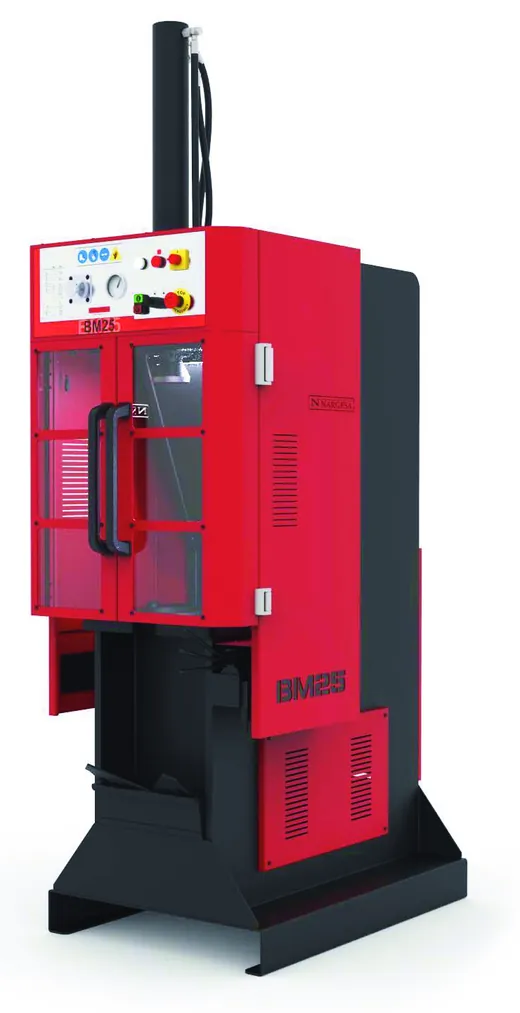
NARGESA BM25
Type: Broaching machineCountry of manufacture: SpainSpindle stroke: 600 mm
PRICE ON REQUESTDetails →
NARGESA BM25 broaching machine for keyways and internal profiles: 10 t force, keyway up to 25 mm, 600 mm stroke, 300 mm throat.
Broaching finishes an existing bore: a broach with progressively higher teeth passes through the hub and cuts a keyway or another internal profile along its full length. The keyway width is set by the broach, so it is the same across a batch without fitting. That is why keyways in pulleys, gears, couplings and bushings are broached rather than slotted or milled — as long as the bore goes all the way through.
The catalog carries the NARGESA BM25: 10 t force, keyway up to 25 mm, 600 mm stroke, 300 mm throat, 24 mm/s working and 54 mm/s return speed, 2.2 kW drive, 850 kg. Under DIN 6885 and GOST 23360 a 25 mm keyway takes the key of an 85–95 mm shaft; narrower keyways are broached on the same machine, each with its own broach.
The bore for broaching is prepared in advance — turned on a lathe or drilled and reamed on a column drilling machine. A keyway in a hardened part or a complex through profile is cut by a wire EDM machine, and internal gear rims are cut by gear shaping machines. All machines for holes are in the drilling machines.
The broach passes through the bore in one or a few strokes, so a part takes tens of seconds instead of minutes on a slotting machine. The keyway width is the same across the batch because the tool sets it. Slotting is needed when the keyway is blind or there is no broach for the size.
Broaching continues the machining of a bore after drilling and boring, so the machine sits next to the drilling machines.
A drawing of the part with the keyway, the material and hardness, the bore diameter and length, and the number of parts per month. We will choose the broaches and bushings and prepare a quotation with delivery.
Send your part parameters — we'll select and quote.